Solutions · Industry Solutions
Textile dyeing & finishing: color, salt, and reuse
High COD, color, and salt from dyeing: coagulation, oxidation, MBR/UF pretreatment, and RO for high-quality reuse with antiscalant discipline.
Use when
Salt and dye hydrolysates foul membranes; reuse targets collide with variable batch discharges.
Process options
Primary color removal, biological steps where BOD allows, UF/MBR polish, and staged RO with chemistry tuned to sulfate/silica.
Assessment output
Permeate quality matched to wash steps, lower freshwater withdrawal, and measured discharge performance.
Inputs and conditions for an assessment
Collect feed variability, capacity, target quality, operating hours, discharge or reuse boundaries and installed equipment data. Compare examples on matched conditions and meter boundaries; assess a project using actual water data, equipment documentation and any necessary tests.
View the process illustration
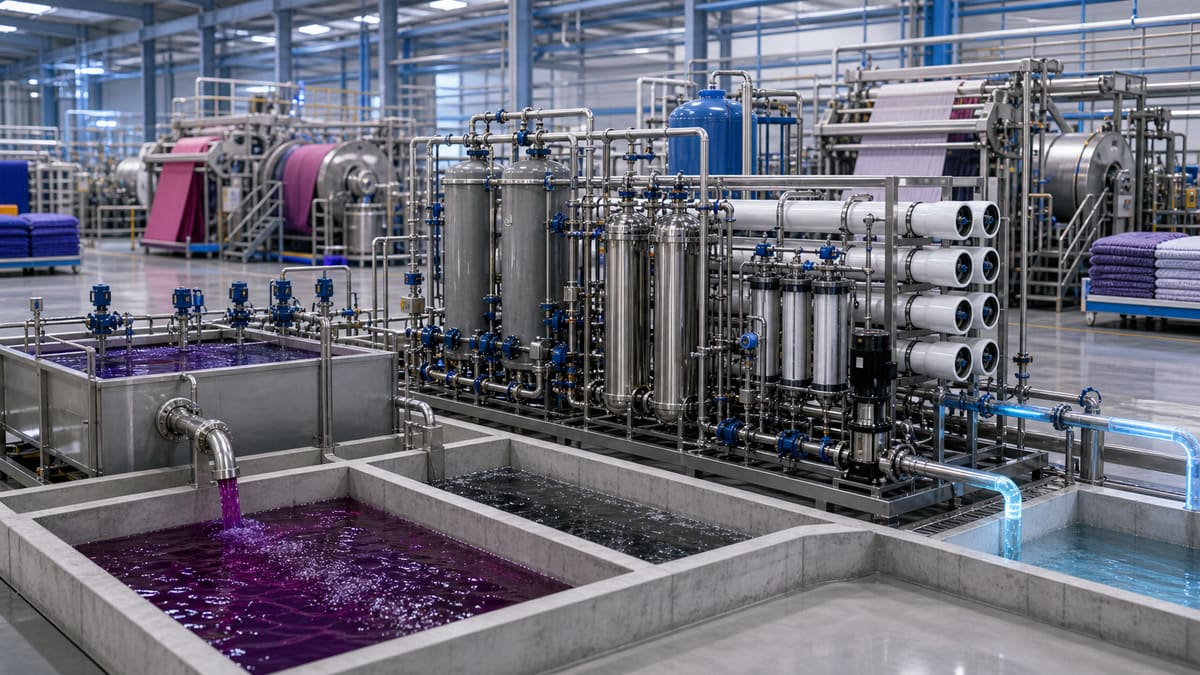
Textile Dyeing & Finishing Wastewater Treatment: A Sustainable Approach to Color, Salt, and Reuse
The textile dyeing and finishing industry is a critical global sector, yet it is highly water-intensive and generates complex wastewater streams. These effluents are characterized by significant concentrations of chemical oxygen demand (COD), color (chromaticity), high salinity (primarily chlorides and sulfates from reactive dyes and fixing agents), surfactants, and often heavy metals. The inherent batch variability in dyeing processes, driven by different fabric types, dye recipes, and production schedules, presents substantial challenges for consistent wastewater treatment and especially for water reuse initiatives.
Water Quality Targets for Reuse
- Dye Bath Makeup: Illustrative project targets are conductivity < 50 µS/cm, color < 10 ADMI units, TSS < 1 mg/L, and low COD (< 20 mg/L); validate them against the actual dye recipe and color consistency trials.
- Washing & Rinsing: Illustrative targets are conductivity < 20-30 µS/cm and color < 5 ADMI units; suspended-solids acceptance must specify a measurement and detection limit rather than absolute zero.
- General Utilities (Cooling Towers, Boiler Feed): Conductivity < 100 µS/cm for cooling and hardness < 1 mg/L and silica < 0.1 mg/L for boiler makeup are example targets, not universal ASME/IAPWS limits; use the actual cooling chemistry, boiler pressure, steam duty, and equipment requirements.
- RO Feedwater Quality: SDI₁₅ < 3 and TSS < 1 mg/L can be project targets, subject to the selected reverse osmosis membrane's feed specification; low SDI alone does not control dissolved-organic, biological, or scaling risks.
Integrated Process Train for Textile Wastewater Reuse
-
Primary & Secondary Treatment:
- Equalization: Critical for buffering the highly variable flow rates, pH, and pollutant loads from batch processes.
- Physicochemical Treatment: Coagulation, flocculation, and sedimentation/dissolved air flotation (DAF) are employed for bulk removal of TSS, color, heavy metals, and a significant portion of COD.
- Biological Treatment: Aerobic or anaerobic biological processes are implemented where biodegradable organic loads (BOD) are high and amenable to biological degradation, provided toxicity levels permit stable biomass.
- Advanced Oxidation Processes (AOPs): For particularly recalcitrant organic compounds and persistent color, AOPs like ozone, Fenton, or photo-Fenton can be integrated to further reduce COD and improve biodegradability.
-
Advanced Fine Filtration (Pre-RO): For textile effluents with high TSS, colloids, or fluctuating organic loads, test whether multimedia filtration (MMF) meets the selected RO feed specification. Ultrafiltration (UF) or a membrane bioreactor (MBR) may provide a stronger solids barrier before reverse osmosis. UF/MBR performance depends on membrane integrity and operating conditions; verify SDI₁₅ < 3 if adopted as the project target, and separately manage dissolved organics, biological activity, and RO concentrate scaling.
Operations, Monitoring, and CIP Philosophy
Sustained membrane performance requires monitoring of normalized production, salt passage, pressure loss, and cleaning results. Define alarms and cleaning criteria for the selected membrane and actual operating conditions.
Risks and Common Engineering Mistakes
Common mistakes include sizing from average batch quality alone, treating low SDI as proof that all fouling risks are controlled, and omitting a route for concentrated salts and cleaning waste.
Digital Operations & Maintenance (O&M)
Specify the measurements and responsibilities required for remote monitoring: flow rates, pressures (including stage ΔP), conductivity, temperature, and chemical dosing. Review trends in normalized permeate flow and transmembrane pressure, confirm instrument calibration, and compare cleaning results before changing CIP timing. Any prediction or remote intervention needs validation against the actual plant and agreed access and response arrangements.
Reference: DuPont FilmTec technical manual: feed quality, pretreatment, and fouling control.
Related equipment & product lines
These categories typically support the approach above—open any line to compare brands and models.
- ChemicalsAntiscalants, cleaners, and process chemicals for water treatment operations.View category →
- RO MembranesReverse osmosis membrane elements for municipal and industrial desalination.View category →
- UF ModulesUltrafiltration modules for suspended solids and colloid removal.View category →
- Ozone GeneratorOzone generation systems and peripherals for advanced oxidation processes.View category →
For a closer review, use the engineering inquiry form to share feed, capacity, target, and project stage. Submission does not constitute a completed design or performance commitment.