Solutions · Industry Solutions
Lithium-ion battery manufacturing: aqueous electrode processing and cleaning water
Water for cell manufacturing: strict metal-ion limits, low TOC, and RO/EDI polishing for mixing, washing, and cleanroom-adjacent loops.
Use when
Trace transition metals and organics in water can catalyze unwanted side reactions and affect slurry stability—limits are tight even when resistivity looks fine.
Process options
High-performance pretreatment, RO (often staged), EDI or mixed-bed polishing, and hygienic materials of construction for critical loops.
Assessment output
Repeatable slurry and washing quality with monitoring aligned to the ions that actually affect cell chemistry.
Inputs and conditions for an assessment
Collect feed variability, capacity, target quality, operating hours, discharge or reuse boundaries and installed equipment data. Compare examples on matched conditions and meter boundaries; assess a project using actual water data, equipment documentation and any necessary tests.
View the process illustration
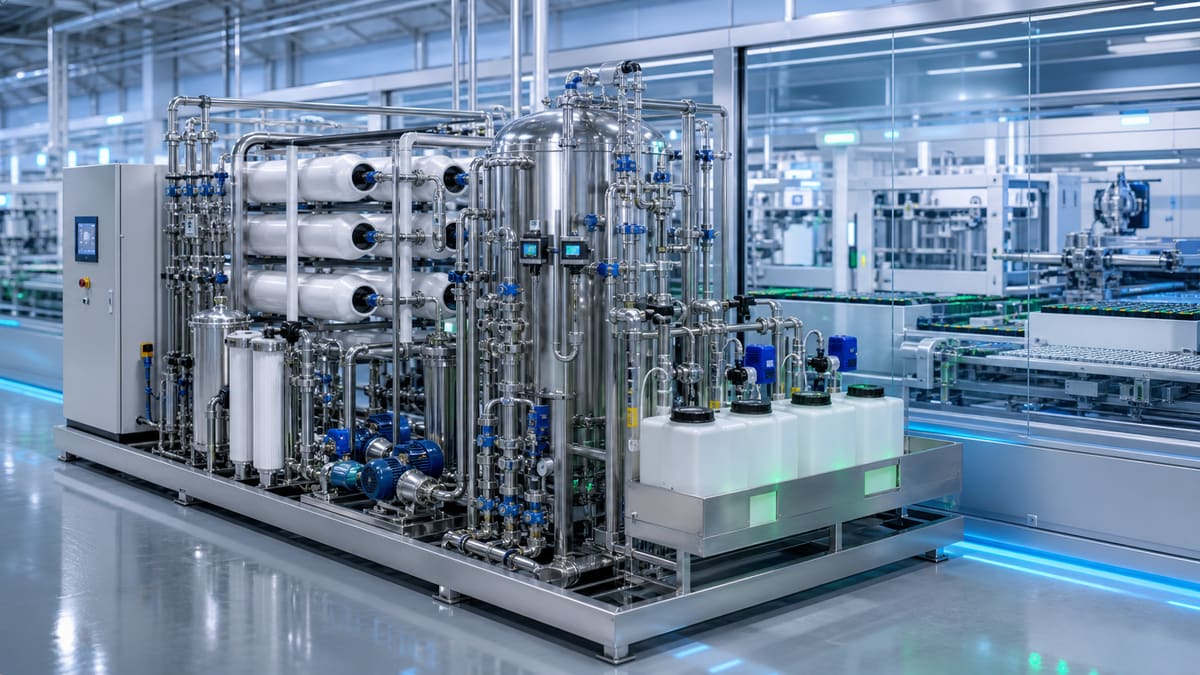
Lithium-ion battery manufacturing: aqueous electrode processing and cleaning water
Lithium-ion battery plants may use water for specified aqueous electrode dispersions, washing and utilities; other electrode routes use solvents such as NMP. Conventional nonaqueous electrolytes require moisture control and must not be treated as receiving ordinary process water. Define each loop with the electrode/electrolyte supplier. Trace metals such as Fe, Cu, Zn, calcium, magnesium and total organic carbon (TOC) can affect suitable aqueous processes, but allowable limits and consequences depend on cell chemistry, binder and process. Separate water-transfer and cleanroom requirements from dry-room/electrolyte moisture specifications.
Industry Challenges and Regulatory Drivers
Quality, cost and environmental requirements must be set for the actual battery process. ASTM D5127-13 Standard Guide for Ultrapure Water Used in the Electronics and Semiconductor Industries and Type E-1.2 can inform an agreed comparison, but are not universal battery-water standards or automatic regulatory compliance. Establish a supplier-approved water specification and applicable discharge permit.
Water Quality Targets for Battery Manufacturing
The following values are illustrative candidate specifications, not universal battery requirements. Confirm the loop, temperature, sampling method and required analytical sensitivity:
- Resistivity: Example >10 MΩ·cm, with critical targets approaching 18.2 MΩ·cm at 25 °C; do not specify above the pure-water ionic limit. ASTM D5127-13 Type E-1.2 does not alone qualify battery water or authorize adding water to a nonaqueous electrolyte.
- TOC (Total Organic Carbon): <50 µg/L, often targeting <10 µg/L for critical applications.
- Particles: <1 particle/mL at >0.2 µm.
- Trace Metals (e.g., Fe, Cu, Zn, Ca, Mg): <1 ppb each.
- Silica: <5 ppb.
- Microbial Count: <1 CFU/100 mL.
Process Train: From Raw Water to Specified Process Quality
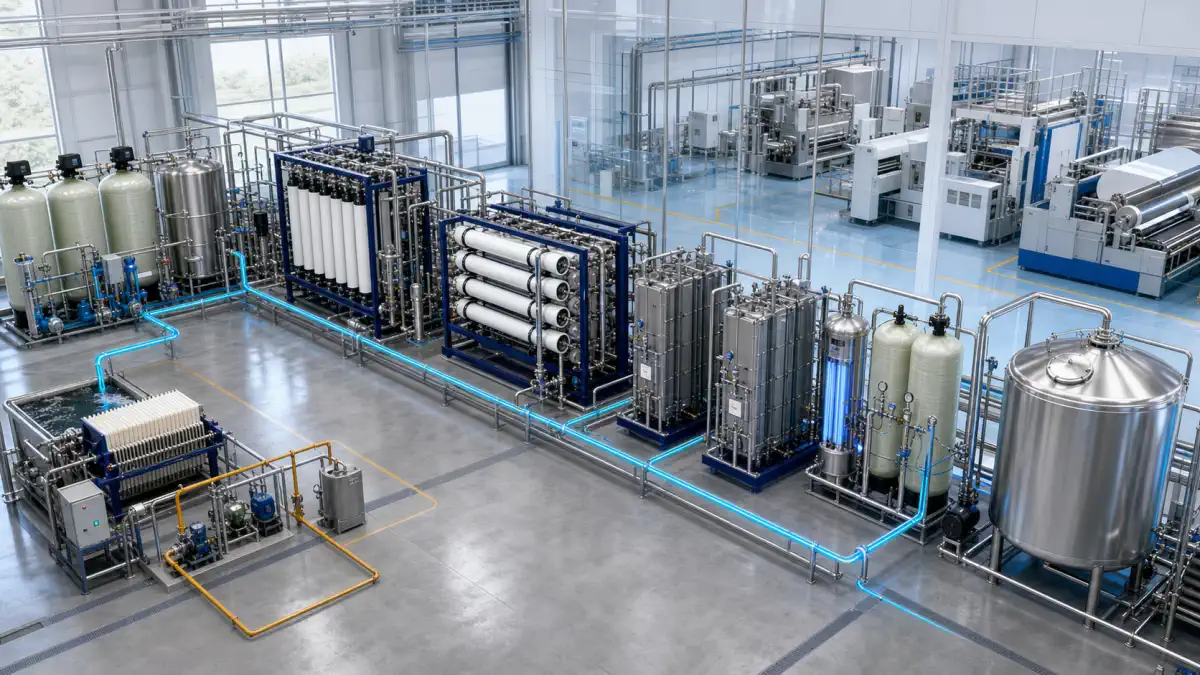
- Raw Water Pretreatment:
- Multimedia Filtration (MMF): Assess raw-water particles and turbidity. SDI₁₅ over 15 minutes consistently above 5 indicates a pretreatment concern for selected RO products, not a universal mandate to install MMF rather than another validated route.
- Ultrafiltration (UF): Assess UF for particles and colloids. Microbial removal, particularly viruses, requires product-specific validation and integrity control; UF does not universally ensure SDI <3, optimum RO operation or longer membrane life. Verify net output and downstream trends.
-
Antiscalant Dosing: Select compatible control for the actual concentrated salts; dosing does not universally prevent RO scaling.
-
Dechlorination: Sodium bisulfite or activated carbon filtration removes free chlorine to protect polyamide RO membranes from oxidation.
- Cartridge Filtration: Select a final RO guard filter, for example 5-micron absolute where required by the membrane manufacturer; nominal and absolute ratings are not interchangeable.
-
Reverse Osmosis (RO):
- Select RO elements for measured feed and target quality, balancing recovery, flux, concentration polarization and scaling. LSI assesses calcium carbonate, not silica or every salt. Evaluate silica separately. Double-pass RO means first-pass permeate feeds the second pass, distinct from two concentrate stages; below 5 µS/cm is a conditional target, not a guarantee.
-
EDI Polishing (Continuous Electrodeionization):
- Feed suitable RO permeate to EDI within specified conductivity-equivalent, hardness, silica and other limits. A DC field and membranes transfer ions to concentrate while water splitting regenerates resin without routine acid/caustic regeneration. Electrode flush and gases require the actual manufacturer arrangement, and cleaning or concentrate handling remains necessary. >16 MΩ·cm is a conditional quality example, not full UPW acceptance.
-
UV Sterilization and Polishing:
- UV Oxidation (185 nm): Can support TOC reduction through oxidation, but not every organic is fully converted to CO₂ and water. Verify dose, actual removal, downstream ionic polishing and measured TOC.
- UV Disinfection (254 nm): Validate the reactor dose, transmission and microbial reduction. UV has no persistent residual and does not alone guarantee loop microbial control.
- Polishing Mixed-Bed Ion Exchange (Optional): For achieving 18.2 MΩ·cm resistivity and ultra-low ionic impurity, a non-regenerable mixed-bed ion exchange polisher or dedicated resin columns may follow EDI, often placed just before the point of use.
Operations, Monitoring, and CIP Philosophy
Set monitoring and maintenance from the installed system and the approved battery-process specification. Define sampling locations, calibration and action criteria instead of assuming an existing integrated instrumentation platform:
- Transmembrane Pressure (TMP): Monitored across UF and RO membranes to detect fouling trends.
- Normalized Permeate Flow (NPF): Normalize RO trends for relevant temperature, pressure, salinity and recovery changes. A trend alone does not uniquely establish degradation or fouling.
- Conductivity and Resistivity: Monitored at every critical stage (post-RO, post-EDI, point of use) to ensure ionic purity.
- TOC Analyzers: Online TOC meters provide continuous assurance for organic purity in critical loops.
- Differential Pressure (ΔP): Across all filtration stages to indicate filter loading.
Use Cleaning-in-Place (CIP) criteria for the actual membrane based on normalized flow/salt passage and pressure drop, with operator approval and compatible procedures. NPF, TMP and ΔP trends support review but cannot guarantee cleaning precedes every irreversible event. Verify post-cleaning performance.
Risks and Common Engineering Mistakes
- Underestimating Raw Water Variability: Failing to conduct comprehensive long-term raw water analysis is a common pitfall, leading to undersized pretreatment or inadequate chemical dosing.
- Overlooking Trace Contaminants: Conductivity and TOC alone can miss relevant metals. Develop a detailed User Requirements Specification (URS) with electrode and electrolyte suppliers, including the water-bearing loops and separate moisture-exclusion requirements.
- Improper Materials Selection: Using non-specified materials (e.g., brass fittings, inappropriate plastics) introduces leachables that can poison sensitive battery chemistries.
- Insufficient Recovery Rate Planning: Evaluate RO concentrate mass balance, LSI for carbonate and other salts separately; select compatible control and verify operating limits rather than expecting an antiscalant to guarantee freedom from scale.
- Ignoring Biofouling: Inadequate UV, regular sanitization, or poorly designed loops can lead to microbial growth, impacting both water quality and membrane performance.
Engineering Tip
Ask electrode and electrolyte suppliers for a written maximum allowable list for metals and TOC per loop, not a single plant-wide “DI water” specification. This granularity is crucial for optimizing system design and cost.
Frequently Asked Questions
Q: Do we need double-pass RO everywhere? A: Rarely. Double-pass RO is typically employed where specific contaminant removal, such as high boron rejection, or exceptionally low ionic leakage is critical and economically justified. For many applications, a well-designed single-pass RO followed by EDI is sufficient.
Q: How important is TOC? A: TOC can be very important for the binder and dispersion chemistry of specified aqueous slurries. Nonaqueous electrolyte chemistry has separate contaminant and moisture requirements. Specify where water TOC is measured, for example post-UV or point of use, and how often, using a validated method for the agreed limits.
Q: Can we share water with cooling towers? A: Never without clear physical and control separation. The risk of cross-contamination from cooling tower water, which is often chemically treated and prone to microbial growth, is far too high and could have catastrophic consequences for battery production quality. The saved pump head or pipe run is not worth the immense risk.
Q: What is the significance of LSI in RO design? A: The Langelier Saturation Index (LSI) indicates the scaling potential of water, primarily for calcium carbonate. In high-recovery RO systems, the concentration of dissolved solids increases significantly in the concentrate stream. Monitoring LSI is critical to predict and prevent calcium carbonate scaling on the membrane surface, which would lead to reduced permeate flow and increased transmembrane pressure. Proper antiscalant dosing and controlled recovery rates are used to maintain LSI within acceptable limits.
References
Related equipment & product lines
These categories typically support the approach above—open any line to compare brands and models.
- RO MembranesReverse osmosis membrane elements for municipal and industrial desalination.View category →
- Electrodeionization (EDI)EDI modules and systems for ultrapure water production.View category →
- Ion Exchange ResinsCation/anion and mixed bed resin solutions for demineralization and polishing.View category →
- UF ModulesUltrafiltration modules for suspended solids and colloid removal.View category →
For a closer review, use the engineering inquiry form to share feed, capacity, target, and project stage. Submission does not constitute a completed design or performance commitment.