Solutions · Industry Solutions
Display & photovoltaic panel cleaning water: high flow, low particle burden
High-volume rinse and cleaning water for displays and PV: particle control, hardness, and RO/UF design for throughput and membrane protection.
Use when
High-flow rinses demand huge water volumes; particles and hardness drive spotting, coating defects, and rapid RO fouling if pretreatment is undersized.
Process options
Multimedia or UF pretreatment, single-pass RO for demineralization, and loop sanitation discipline—with flux and recovery chosen for water cost, not hero recovery.
Assessment output
Stable rinse quality at design throughput, fewer unplanned RO cleans, and predictable makeup water chemistry across shifts.
Inputs and conditions for an assessment
Collect feed variability, capacity, target quality, operating hours, discharge or reuse boundaries and installed equipment data. Compare examples on matched conditions and meter boundaries; assess a project using actual water data, equipment documentation and any necessary tests.
View the process illustration
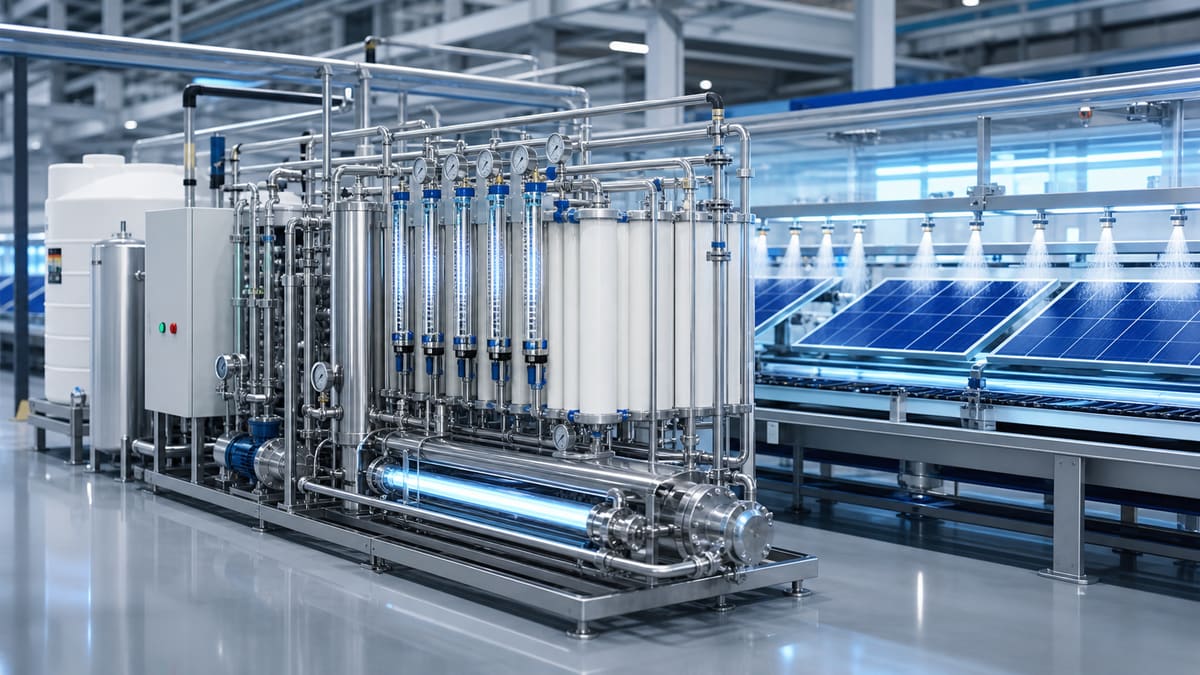
Display & Photovoltaic Panel Cleaning Water: High Flow, Low Particle Burden
Display and photovoltaic (PV) manufacturing use water for specified cleaning and rinse steps. Define particles, ions, organics and other contaminants at the actual process point; different steps do not share a universal UPW requirement. ASTM D5127-13 is an electronics-water guide, with recommendations at the point of distribution, not an automatic legal limit or qualification for every display/PV process. Select the applicable edition and process specification rather than treating Type E-1.2 as a generic resistivity grade.
The economic ramifications of suboptimal water treatment are substantial. Beyond the direct cost of makeup water, manufacturers face losses from increased blowdown rates, premature membrane replacement, and costly rework or scrap. A common challenge arises when system designs prioritize theoretical recovery rate without adequately addressing feed water quality variability, such as seasonal spikes in SDI (Silt Density Index) or organic load. Such oversights can lead to excessive concentration polarization on membrane surfaces, forcing frequent, unscheduled CIP (Clean-in-Place) cycles, which undermine the economic justification for aggressive water conservation strategies.
Industry Context & Regulatory Drivers
The global demand for high-performance displays and efficient solar cells continues to escalate, driving innovation in manufacturing processes that require ever-more stringent control over contamination. Water is used in numerous stages, from wafer slicing and substrate cleaning to chemical mechanical polishing (CMP) and final rinsing. Each step presents unique water quality demands.
Water Quality Targets
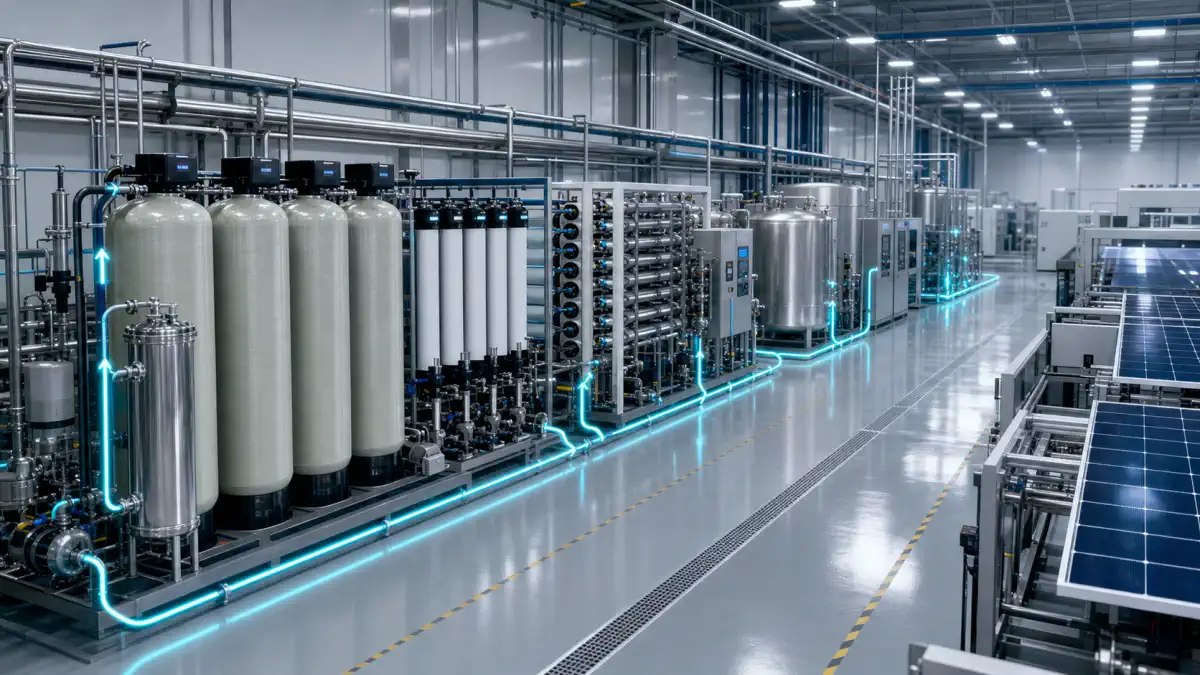
The following values are illustrative project targets, not universal display/PV requirements. Establish the process specification, sample location, temperature, analytical method and detection limit, then validate water quality against actual yield needs:
- Conductivity/Resistivity: Example general-rinse target below 1 µS/cm; selected critical-process targets above 10 MΩ·cm, approaching 18.2 MΩ·cm at 25°C. Conductivity alone does not establish complete UPW quality.
- Particles: Extremely low particle counts, often specified by particle size and quantity (e.g., <100 particles/mL @ >0.2 µm).
- Total Organic Carbon (TOC): Typically <50 ppb for general use, and <5 ppb for critical applications.
- Hardness: Effectively zero (<0.01 mg/L as CaCO₃) to prevent spotting and scaling.
- Silica: <20 ppb and <5 ppb are example high-purity targets at specified locations, not a universal RO-feed ceiling or guarantee for permeate. Evaluate actual feed/concentrate silica, pH, temperature, recovery and product limits separately.
- Dissolved Gases: Often degassed (e.g., <20 ppb O₂) for certain sensitive processes.
- Microbial Count: <10 Colony Forming Units (CFU)/100mL for bulk, and non-detectable for critical points of use.
1. Pretreatment – Safeguarding Downstream Processes
The initial stages are crucial for protecting sensitive membrane technologies and ensuring consistent feed water quality.
3. Electrodeionization (EDI) – Continuous Polishing
For applications with a defined high-resistivity requirement, Continuous Electrodeionization (EDI) can polish suitable RO permeate. It combines resin, ion-selective membranes and a DC field to avoid routine acid/caustic resin regeneration. Confirm feed limits, concentrate/electrode flows, cleaning and end-use quality.
- Mechanism: The field drives ions through resin and selective membranes into the concentrate compartment. Water splitting supports continuous resin regeneration; electrode compartments have separate reactions, gas handling and manufacturer-specific flush arrangements. EDI does not eliminate all maintenance downtime or chemical cleaning.
- Benefits: EDI can meet selected ionic-quality targets, for example >10 MΩ·cm under specified conditions. Compare actual power, feed treatment, cleaning, residual management and whole-life cost; avoiding routine regenerants does not guarantee lower total cost or environmental impact.
4. Post-Treatment & Distribution – Maintaining Purity
The final stages ensure the water maintains its purity until the point of use.
Operations, Monitoring, and CIP Philosophy
Set monitoring and maintenance from the installed equipment and water specification. Normalize RO performance, inspect pretreatment, validate point-of-use quality and use manufacturer-approved CIP procedures; measure actual uptime and operating costs.
Risks and Common Engineering Mistakes
Several factors can jeopardize the efficiency and reliability of display and PV water treatment systems:
- Underestimating Raw Water Variability: Failing to account for seasonal or episodic changes in raw water quality (e.g., turbidity, organics, temperature) can lead to rapid fouling of pretreatment and RO membranes, resulting in frequent CIPs or premature membrane replacement.
- Aggressive Recovery Without Scale Assessment: Evaluate recovery rate, LSI for calcium carbonate, and separate silica/sulfate/other scale risks. Select compatible antiscalant or other control as required; high recovery can raise scaling risk but neither LSI nor dosing guarantees control of every deposit.
- Inadequate Pretreatment: Skipping or undersizing UF or MMF when the SDI of the raw water is consistently high directly exposes RO membranes to particulate fouling, drastically shortening their lifespan.
- Poor Distribution System Design: A highly purified water source can be recontaminated by an improperly designed or maintained distribution loop. Stagnant zones, inappropriate materials, or insufficient flushing can lead to microbial growth or particle shedding.
- Neglecting TOC Control: For thin-film applications, high TOC can lead to defects. Without UV oxidation or specific TOC removal resins, even high-resistivity water may not be suitable.
References
Related equipment & product lines
These categories typically support the approach above—open any line to compare brands and models.
- UF ModulesUltrafiltration modules for suspended solids and colloid removal.View category →
- RO MembranesReverse osmosis membrane elements for municipal and industrial desalination.View category →
- Sediment FiltersPre-filtration cartridges and housings for suspended solids removal.View category →
- Pumps & PumpingHigh-pressure and process pump solutions for water treatment skids and plants.View category →
For a closer review, use the engineering inquiry form to share feed, capacity, target, and project stage. Submission does not constitute a completed design or performance commitment.